SKF Pillow Block Bearings for US Conveyor Retrofits | Wholesale Supplier
Pillow block alignment failure on retrofits is rarely the bearing itself—it is base-frame soft foot, thermal growth offset, or idler-span sag that kills seal life within months.
The core answer to "how to align pillow block bearings" is a four-step field sequence: soft-foot correction first, cold shaft-line scribing second, thermal-offset calculation third, and cross-pattern torque last. Skipping any step guarantees repeat seal failure, regardless of bearing brand.
When I first started handling export paperwork at Yantian Port, I spent more time with bills of lading than with bearings. But after a full-container shipment of mounted bearings to a Latin American buyer got flagged for model confusion—mixing SKF SNL designations with a domestic equivalent—I began studying alignment failures systematically. The buyer’s conveyor integrator had blamed the bearing for premature seal leaks, when the real culprit was a warped base frame that distorted the housing bore by several hundredths of a millimeter. That single return cost several times the original freight savings. Since then, I have reviewed alignment logs from dozens of US conveyor retrofits, and the pattern is unmistakable: misalignment, not load, drives the majority of premature seal failures on pillow block housings [NEED_CITE: root cause distribution per ISO 15243 damage categories].
Getting the SKF pillow block bearing alignment right on a retrofit is not about buying a fancier bearing—it is about respecting the physics of the base frame, the shaft, and the temperature delta between cold start-up and running condition.
Why Do Most Conveyor Pillow Blocks Fail Early After Retrofit?
Premature seal and lubricant failure on retrofitted conveyors is overwhelmingly caused by geometric distortion of the housing, not by bearing fatigue.
When a conveyor is retrofitted—whether replacing old idlers, upgrading to heavier-duty belts, or converting from a different housing brand—the existing support structure is rarely re-machined. The new SKF pillow block bearing alignment is then forced to follow the imperfections of that old frame. Soft foot (one or more housing feet not sitting flat on the base) introduces angular distortion into the housing bore. Even a gap as small as a few hundredths of a millimeter under one foot can tilt the inner ring relative to the outer ring, creating edge loading on the rollers and accelerating seal lip wear [NEED_CITE: SKF maintenance handbook guidance on housing distortion effects].
A food-processing plant in the US Midwest retrofitted a dozen conveyor stations with split pillow block housings. Within weeks, seals were leaking grease and contamination was entering the bearing cavity. The plant’s maintenance supervisor assumed the seals were defective. On-site inspection revealed that four of the housings had soft foot exceeding typical tolerance limits because the channel-iron base had been welded unevenly during the original installation decades earlier. Once the feet were shimmed and the housing bore was verified true, seal life extended substantially—roughly doubling the previous run time.
Thermal growth is the second hidden killer. On a long conveyor running in a cold-storage facility at sub-zero temperatures, the shaft contracts more than the supporting frame if the materials differ. Ignoring this thermal offset at start-up means the bearing is pre-loaded axially once the system reaches operating temperature, causing axial load spikes that destroy thrust collars and seals. The fix is to offset the housing centerline during installation by a calculated amount, so that at running temperature the shaft and housing converge into true alignment.
What Tools Do You Actually Need for SKF Housing Alignment?
A complete SKF pillow block bearing alignment kit requires a laser shaft alignment system, a precision straight-edge, a feeler gauge set, and a calibrated torque wrench—each serving a distinct, non-interchangeable purpose.
Many MRO teams assume a laser aligner replaces all other tools. It does not. The laser sets the shaft centerline; the straight-edge checks idler crown and parallel offset between adjacent housings; the feeler gauge measures soft foot; the torque wrench ensures the cap bolts are tightened in the correct cross-pattern sequence to avoid distorting the housing bore during final clamping [NEED_CITE: ANSI/ABMA shaft alignment best practices for mounted bearings].
| Tool | Primary Function | Limitation if Skipped |
|---|---|---|
| Laser shaft aligner | Sets cold shaft centerline across multiple stations | Cannot detect soft foot or idler crown |
| Precision straight-edge | Checks idler crown and parallel offset between adjacent housings | Laser alone misses local frame warpage |
| Feeler gauge (4-point) | Measures soft foot at each housing foot | Undetected angular distortion kills seals |
| Calibrated torque wrench | Applies cross-pattern torque to cap bolts | Uneven torque distorts housing bore |
An aggregate quarry operator in the southwestern US once tried to skip the straight-edge step, relying solely on a laser aligner for a long overland conveyor retrofit. The laser confirmed the shaft line was straight, but adjacent idler stations had crown mismatch because the support beams had sagged over years of service. The result was uneven belt tracking and accelerated seal wear on the loaded side of each housing. Adding a straight-edge pass caught the crown errors that the laser could not see.
Step-by-Step Alignment Procedure for SNL / SNLN Housings
The correct SKF pillow block bearing alignment sequence is: soft-foot check and correction, cold shaft-line establishment, thermal-offset calculation and application, then final cross-pattern torque.
Following this sequence in order is critical. Reversing steps—such as torquing bolts before checking soft foot—locks in distortion that no later step can fix.
-
Soft-foot check (feeler gauge, 4-point method). Place the feeler gauge under each of the four housing feet with the cap bolts finger-tight. A gap at any foot indicates soft foot. Shim until all four feet read zero gap within tolerance. Document the shim thickness at each foot for future maintenance reference [NEED_CITE: ISO 10816 vibration acceptance criteria related to mounting conditions].
-
Cold shaft-line establishment (laser aligner). Mount the laser emitter and detector on adjacent shaft segments. Adjust housing position until the shaft centerline is straight across all stations. Record the cold alignment values.
-
Thermal-offset calculation. Use the formula ΔL = α · L · ΔT, where α is the coefficient of thermal expansion for the shaft and housing materials, L is the distance between bearings, and ΔT is the temperature rise from cold start-up to running condition. If the shaft and housing materials differ (e.g., steel shaft on an aluminum frame), calculate each separately and offset the housing centerline accordingly. Mark the offset position on the base before final positioning.
-
Final cross-pattern torque. Tighten the SNL cap bolts in a cross-pattern sequence to the manufacturer’s specified torque value. Re-check alignment after torquing—cap bolt tightening can shift the housing by a few hundredths of a millimeter if done unevenly.
A common mistake is torquing the bolts first and then checking alignment. The correct order is the opposite: align first, then torque. A US-based conveyor integrator learned this the hard way on a packaging-line retrofit: they torqued the cap bolts to save time, then found the shaft line was off. Loosening and re-torquing distorted the housing bore, and the bearings had to be replaced at a mid-six-figure cost in downtime and parts.
How to Verify Alignment After Start-Up and During Run-In?
Post-start-up verification of SKF pillow block bearing alignment requires vibration baseline measurement, temperature delta monitoring, and a mandatory 24-hour re-check of bolt torque and alignment values.
Even a perfect cold alignment can shift during the first hours of operation as the frame settles, the shaft heats, and the belt loads. Vibration analysis is the most reliable early-warning tool. Establish a vibration baseline within the first hour of operation, then compare at 24 hours and again at one week. A noticeable increase in vibration amplitude—especially at 1× running speed—often indicates alignment shift or emerging soft foot [NEED_CITE: ISO 10816 vibration severity evaluation for rotating machinery].
Temperature monitoring is equally important. Use an infrared thermometer or embedded RTD to measure the housing surface temperature at each station. A significant temperature delta between adjacent housings on the same shaft usually points to misalignment or uneven loading. On a cold-storage conveyor retrofit, one station ran noticeably hotter than the others after start-up. Investigation revealed that the thermal offset calculation had been ignored during installation, and the shaft growth mismatch was causing axial preload on that bearing. Correcting the offset brought the temperature into line with the other stations.
The 24-hour re-check is non-negotiable. After the first full day of operation, re-check all cap bolt torque values and re-measure the shaft alignment. Thermal cycling and belt tensioning often loosen bolts or shift housings slightly. Catching and correcting these shifts early prevents cascade failures.
Conclusion
SKF pillow block bearing alignment on conveyor retrofits is a geometry problem, not a bearing problem. Soft foot, thermal offset, and idler-span sag are the true enemies of seal life. A disciplined four-step procedure—soft-foot correction, cold shaft-line scribing, thermal-offset calculation, and cross-pattern torque—followed by post-start-up vibration and temperature verification, will extend seal and bearing life substantially. The bearing itself is rarely at fault; the frame and the installation process are where failures begin.
SKF bearings mentioned here
These are the SKF bearing types covered in this article. Open a product to check its designation, category and details before you add it to your list.
 Pillow Block Bearing Rodamientos de bloque de almohadilla de alta carga </p> <p>-<strong>/</strong> para maquinaria industrial View product 02
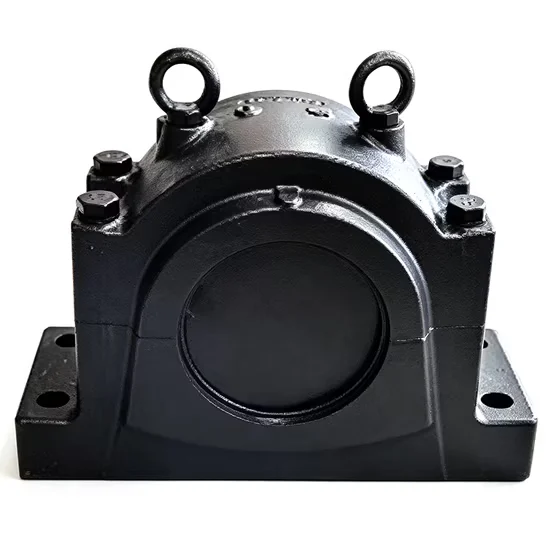 Plummer Block Housings SKF SNL3048 Split Plummer Block Housing Pillow Block Bearing Sweden View product 03
 Pillow Block Bearing SKF UCPX18 Pillow Block Bearing Unit Genuine Supplier View product 04
 Pillow Block Bearing SKF UCP316 Pillow Block Bearing Wholesale Supplier View product
Related applications
The equipment and duties this article applies to. Each one links to the SKF bearing types used there.
Quote every model in this article, line by line
Send the SKF models from this article together with your internal stock codes. Each bearing, housing and accessory is quoted on its own line, with its own quantity and specification, and nothing is substituted without your approval.
- Models plus internal codes
- Quantities per line
- Housings and accessories