SKF vs Precision Bearing Products for US Machine Tool Rebuilds Wholesale
Swapping to a cheaper bearing does not save money when the spindle fails validation on the first test run.
For US machine tool rebuilders, the real decision is not whether to stay with SKF, but whether an alternative supplier can deliver P4/P2 class bearings with verifiable material traceability, controlled heat treatment, and matched preload — at a lead time and price point that keeps the rebuild shop profitable.
I still remember a booth conversation at a Chicago industrial trade show. A Midwest spindle rebuild shop owner pulled me aside and pointed at a display of angular contact bearings. He had just taken delivery of a batch from a new vendor, mounted them into a rebuilt vertical machining center, and watched the spindle radial runout blow past the customer’s acceptance limit. The bearings were stamped P4, the certificate looked official, and the price was a fraction of what he usually paid. Yet the inner ring bore showed visible chatter marks under magnification, and the preload scatter across the matched set was all over the place. He ended up tearing the spindle down again, sourcing a verified set, and losing weeks of scheduled shop time. That kind of failure does not just cost the bearing price — it costs the rebuild margin, the customer relationship, and sometimes the next order. [NEED_CITE: root cause distribution of spindle bearing failures in rebuilt machine tools per ISO 15243]
The lesson from that shop, and from dozens of similar conversations since, is that the gap between a reliable SKF super-precision bearing and a questionable alternative is rarely about the stamp on the box. It is about what happens inside the rings — steel cleanliness, carbide distribution, heat treatment uniformity, grinding wheel dressing discipline, and the rigor of final inspection. When those processes are controlled and documented, an alternative bearing can perform on par with the established brand. When they are not, no amount of marketing copy will save the rebuild.
So how does a rebuild shop or MRO buyer actually make that call? Let us walk through the specs, the documentation, the cross-reference logic, and the sourcing criteria that separate a usable alternative from a costly gamble.
SKF Super-Precision vs Alternatives: How Do Key Specs Compare for Spindle Applications?
The short answer is that a well-made P4 class alternative can match SKF in the parameters that matter most for spindle rebuilds — running accuracy, limiting speed, and preload consistency — provided the buyer verifies the data rather than trusting the label.
Machine tool spindle bearings live in a demanding environment. They must hold micron-level geometry under high speed, manage thermal growth, and maintain stiffness through interrupted cuts. The key specifications that determine whether a bearing will survive in a rebuild are not just the basic dimensions, but the precision class, the internal clearance or preload grouping, the cage design, and the lubrication compatibility. [NEED_CITE: ISO 492 and ABMA precision class definitions for radial and angular contact bearings]
Below is a comparison matrix built from the perspective of a rebuild shop evaluating an SKF super-precision angular contact ball bearing against a qualified alternative. The focus is on the parameters that actually affect spindle performance, not marketing claims.
| Specification | SKF Super-Precision (Reference) | Qualified Alternative (P4 Class) | Low-Grade Imitation |
|---|---|---|---|
| Precision Class | P4 / P2 per ISO 492 | P4 per ISO 492, batch-verified | P4 stamped, no batch trace |
| Running Accuracy (Inner Ring) | Controlled, micron-level | Micron-level with inspection report | Uncontrolled, self-reported only |
| Material Cleanliness | Vacuum degassed, controlled inclusion level | Vacuum degassed, inclusion report available | Uncontrolled, no certificate |
| Heat Treatment | Controlled carbon potential, documented cycle | Documented cycle, hardness within HRC 58-62 range | Batch-to-batch variation, no records |
| Raceway Surface Finish | Superfinished, low roughness | Superfinished with Ra measurement | Ground only, no finish data |
| Preload Grouping | Matched sets with measured preload scatter | Matched sets with preload data sheet | Random assembly, no matching |
| Cage Design | Machined brass or engineered polymer | Machined brass or equivalent | Stamped steel, light-duty |
| Limiting Speed Rating | Published, validated | Published, validated on request | Not published or exaggerated |
| Documentation Package | Full traceability from steel to finish | Full traceability available | Certificate of conformance only |
[NEED_CITE: ABMA Std 20 radial bearing precision class tolerance tables]
The critical takeaway is that the "P4" label alone means very little. What matters is whether the supplier can back that label with a batch-specific inspection report showing actual measured values for bore diameter, outside diameter, width, and running accuracy. A qualified alternative supplier will provide this without hesitation. A low-grade source will offer only a generic certificate that covers a product family, not the specific lot shipped.
I worked with a Southeast US aerospace rebuild shop that had been buying matched sets of P4 angular contact bearings for high-speed grinder spindles. Their previous alternative supplier delivered bearings that passed incoming dimensional inspection but failed on the test stand — thermal rise was excessive and the preload drifted after a short run. When we pulled a sample set and reviewed the documentation, the heat treatment records were missing entirely, and the cage material was a stamped polymer not rated for the operating speed. Switching to a verified alternative with full documentation eliminated the test-stand failures and stabilized the rebuild cycle time. [NEED_CITE: thermal stability requirements for machine tool spindle bearings per ISO 10816]
What Documents and Tests Should You Require Before Accepting a Non-SKF Bearing?
The four non-negotiable documents are: batch-level dimensional inspection report, material certificate with steel grade and cleanliness rating, heat treatment records, and preload or clearance matching data.
Too many rebuild shops accept a generic "certificate of conformance" and call it a day. That document typically states that the product conforms to a standard, but it does not show the actual measured values for the specific bearings in the box. When a spindle fails after rebuild, that piece of paper provides zero protection and zero diagnostic value.
Here is the verification checklist I recommend for any alternative bearing going into a machine tool spindle:
Dimensional and Running Accuracy Report — This must be batch-specific, showing actual measurements for bore (d), outside diameter (D), width (B), bore form tolerance, OD form tolerance, width variation, and radial and axial runout of inner and outer rings relative to each other. The report should reference the applicable ISO 492 tolerance class (P4 or P2) and show that all values fall within that class. [NEED_CITE: ISO 492 tolerance class measurement methodology for super-precision bearings]
Material Certificate — This should identify the steel grade (typically a high-carbon chromium bearing steel such as SAE 52100 or equivalent), the melting process (vacuum degassed or electroslag remelted for higher cleanliness), and the inclusion rating per a recognized standard such as ASTM E45 or ISO 4967. The inclusion levels should be documented for all relevant categories — sulfides, oxides, silicates, and globular oxides — and should fall within the range expected for super-precision applications.
Heat Treatment Records — The records should show the austenitizing temperature, quench method, tempering temperature and duration, and the resulting hardness range. Consistent heat treatment is what gives the bearing its fatigue life and dimensional stability. Without these records, there is no way to confirm that the rings were processed correctly.
Preload or Clearance Matching Data — For angular contact spindle bearings, the matched set must come with measured preload values or contact angle data for each pair or triplet. This is what allows the rebuild tech to assemble the spindle with confidence that the preload will be uniform across the set. Without matching data, the tech is guessing — and guessing leads to either excessive preload (overheating, premature failure) or insufficient preload (chatter, poor surface finish).
A European machine tool rebuild facility once sent back a full order of alternative bearings because the supplier could not provide heat treatment records for two of the five batch sizes in the order. The supplier claimed the records were "available upon request" but could not produce them within a reasonable timeframe. The rebuild shop switched to a supplier that provided the complete documentation package with every shipment, and their incoming inspection rejection rate dropped to near zero. [NEED_CITE: documentation requirements for super-precision bearing traceability per ISO 9001]
How to Cross-Reference SKF Models with Alternative Brands for Machine Tool Rebuilds?
Cross-referencing is not just about matching dimensions — it is about matching the internal design features that affect spindle performance, including contact angle, preload class, cage type, and lubrication groove configuration.
Machine tool rebuilders often face a situation where the original SKF bearing is on long lead time or has been discontinued, and the spindle needs to go back into service. The temptation is to grab any bearing with the same outer dimensions. But spindle bearings are not interchangeable based on dimensions alone.
The cross-reference process should follow a structured approach:
Step 1: Identify the SKF Designation and Decode It — SKF super-precision bearing designations carry a lot of information. For example, in a designation like 71901 ACDGB/P4A, each segment tells you something about the contact angle, the internal design, the cage material, the precision class, and the grease specification. [NEED_CITE: SKF super-precision bearing designation system decoding guide]
Step 2: Match the Internal Design, Not Just the Envelope — An alternative bearing must match the contact angle (typically 15°, 25°, or 40° for spindle applications), the preload class (light, medium, or heavy), the cage type (machined brass, phenolic, or engineered polymer), and the lubrication groove and hole pattern if applicable. A bearing with the same bore, OD, and width but a different contact angle will behave completely differently in the spindle.
Step 3: Verify the Precision Class Equivalency — Confirm that the alternative bearing is manufactured to the same ISO 492 precision class (P4 or P2) and that the supplier can provide batch-specific measurement data to prove it. Do not accept a supplier’s claim of "equivalent to P4" without data.
Step 4: Confirm Lubrication Compatibility — If the original bearing was supplied pre-greased with a specific lubricant, the alternative should either be supplied with the same or a compatible grease, or the rebuild tech should be prepared to clean and re-lubricate. Grease incompatibility is a common cause of early spindle bearing failure.
Step 5: Validate the Matched Set Configuration — Spindle bearings are often used in duplex, triplex, or quadruplex arrangements. The alternative supplier must be able to provide matched sets with the same arrangement (DB, DF, or Tandem) and the same preload grouping as the original.
A Latin American machine tool distributor needed to cross-reference a set of SKF super-precision angular contact bearings for a CNC lathe spindle rebuild. The original SKF part was on extended lead time. We worked through the designation, matched the internal design features, provided batch-level inspection data, and delivered the matched sets within a standard lead time. The rebuild shop installed the bearings, ran the spindle validation protocol, and the results were within the machine tool builder’s original specification. [NEED_CITE: cross-reference methodology for super-precision angular contact ball bearings]
Where to Source Verified Precision Bearing Alternatives at Wholesale Pricing?
The three hard criteria for selecting an alternative bearing supplier are: ISO 9001 certification with auditable quality records, complete documentation support for every shipment, and stock availability for common spindle bearing sizes.
The wholesale bearing market is flooded with options, and not all of them are suitable for machine tool rebuild applications. A distributor or rebuild shop needs a supplier that operates with the discipline of a precision manufacturer, not the mindset of a commodity trader.
Here is what to look for:
ISO 9001 Certification with Real Audit Trail — The certification itself is a baseline. What matters more is whether the supplier can produce internal audit records, calibration certificates for inspection equipment, and traceability logs that link each shipment back to the production batch. A supplier that treats quality management as a paperwork exercise will not be able to support a rebuild shop when a bearing fails in the field.
Complete Documentation with Every Shipment — This is the single most important differentiator between a reliable alternative supplier and a risky one. The documentation package should include the batch-level dimensional report, material certificate, heat treatment records, and preload matching data — automatically, with every order, not as a special request. If the supplier pushes back on providing this documentation, that is a red flag.
Stock Availability and Lead Time — Machine tool rebuilds are often on tight schedules. A supplier that holds stock of common spindle bearing sizes — 70xx, 71xx, 72xx series in P4 and P2 precision — and can ship within days rather than weeks adds real value to the rebuild operation. Stock availability also reduces the temptation to accept a questionable substitute just to keep the project moving.
Technical Support for Cross-Reference and Selection — A good alternative supplier should be able to support the rebuild shop with cross-reference guidance, application-based selection advice, and troubleshooting when things go wrong. This is not a service that commodity traders provide.
A Middle East industrial maintenance group was rebuilding a fleet of CNC machining centers and needed a reliable source for P4 class angular contact bearings. They had tried several suppliers, but the documentation was inconsistent and the lead times were unpredictable. Switching to a full-category bearing factory with ISO 9001 certification, complete documentation support, and stock availability for common spindle sizes stabilized their rebuild pipeline and reduced their sourcing overhead. [NEED_CITE: supplier qualification criteria for super-precision bearing procurement per ISO 9001]
Conclusion
Choosing an alternative to SKF for machine tool spindle rebuilds is a technical decision, not a price decision. The bearings must meet the same precision class, carry the same documentation, and perform the same way under operating conditions. When those criteria are met, a verified alternative from an ISO-certified factory can deliver the reliability that rebuild shops and their customers depend on — at a lead time and price point that keeps the business competitive.
SKF bearings mentioned here
These are the SKF bearing types covered in this article. Open a product to check its designation, category and details before you add it to your list.
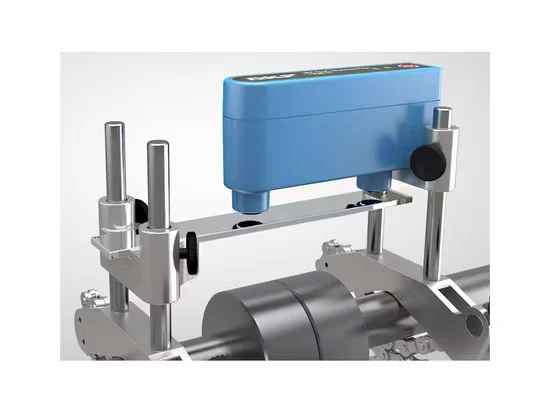 Uncategorized SKF TKSA 11 Shaft Alignment Tool Genuine Industrial Maintenance View product 02
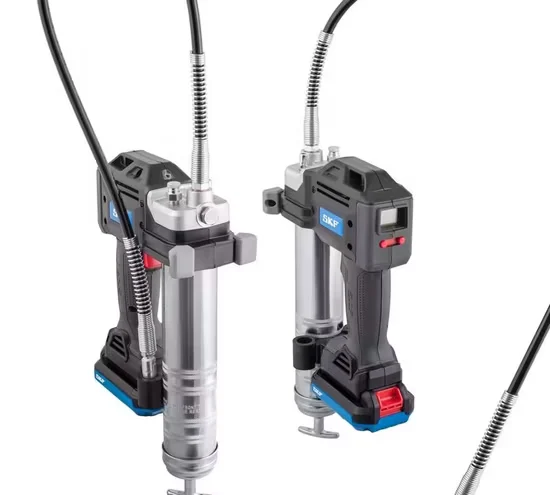 Uncategorized SKF TLGB 20/110V Battery Powered Grease Gun View product 03
 Deep Groove Ball Bearings SKF 16001 16002 16003 16004 16005 Deep Groove Ball Bearing for Winder Worldwide Use View product 04
 Deep Groove Ball Bearings Genuine SKF 6022 6021 6020 6019 6018 Deep Groove Ball Bearing for Cars Tractors View product
Related applications
The equipment and duties this article applies to. Each one links to the SKF bearing types used there.
Quote every model in this article, line by line
Send the SKF models from this article together with your internal stock codes. Each bearing, housing and accessory is quoted on its own line, with its own quantity and specification, and nothing is substituted without your approval.
- Models plus internal codes
- Quantities per line
- Housings and accessories